


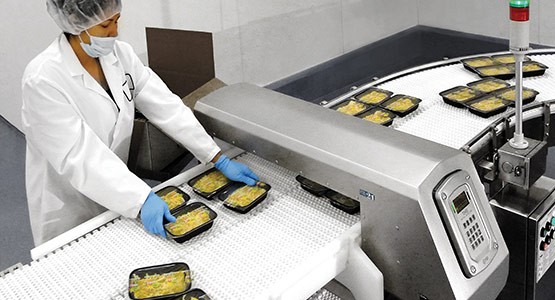

Investing in food metal detection equipment is an important decision for manufacturers that want to improve product safety, meet industry standards, and protect their brand reputation. While the purchase price is a major consideration, businesses should also evaluate other factors that influence the total cost of ownership over the equipment’s lifetime.
Working with a reliable Food Metal Detector Manufacturer can help companies understand different cost factors and select equipment that provides long-term value. A well-designed metal detection system can reduce production risks, minimize waste, and improve overall operational efficiency.
Table of Contents
ToggleInitial Equipment Cost
The initial purchase price is often the first factor businesses consider when selecting metal detection equipment. Costs can vary depending on the type of system, detection technology, size, and additional features.
Factors that influence the initial investment include:
- Equipment design and specifications
- Detection sensitivity requirements
- Conveyor size and configuration
- Automation features
- Customization needs
While lower-cost options may seem attractive, businesses should consider whether the equipment can meet their production demands effectively.
Type of Metal Detection System
Different metal detection technologies come with different cost levels based on their applications.
Common system types include:
Conveyor Metal Detectors
These systems are widely used for packaged and solid food products. Costs depend on conveyor dimensions, speed, and integration requirements.
Gravity-Fall Metal Detectors
Designed for free-flowing products such as powders and grains, these systems may require specialized designs for accurate inspection.
Pipeline Metal Detectors
Used for liquids and semi-liquid products, pipeline systems often involve hygienic designs and integration with processing equipment, which can affect overall costs.
Detection Performance and Technology
Advanced detection capabilities can influence equipment pricing. Systems with higher sensitivity, intelligent signal processing, and automated adjustment features may require a larger investment.
However, improved detection performance can provide long-term savings by reducing false rejects, preventing contamination incidents, and improving quality control.
Customization Requirements
Every production line has unique requirements. Custom features such as special conveyor designs, integration with existing machinery, or specific software functions can increase the overall investment.
Although customized equipment may have a higher upfront cost, it can provide better performance and efficiency when standard solutions do not meet production needs.
Installation and Integration Costs
Installation expenses should be included when calculating the total investment. These costs may involve:
- Equipment setup
- Production line adjustments
- Software integration
- Operator training
- Testing and calibration
Proper installation ensures the system performs correctly and avoids operational issues in the future.
Maintenance and Operating Costs
Long-term expenses are an important part of equipment evaluation. Regular maintenance helps maintain detection accuracy and extends equipment lifespan.
Ongoing costs may include:
- Routine inspections
- Replacement parts
- Calibration services
- Cleaning procedures
- Technical support
Choosing durable equipment with reliable support can reduce maintenance expenses over time.
Energy Efficiency and Productivity
Energy consumption and production efficiency also affect the overall cost of ownership. Modern systems designed for efficient operation can help reduce operating expenses while maintaining inspection performance.
Equipment that integrates smoothly into production lines can also reduce downtime and improve workflow efficiency.
After-Sales Support and Service
Technical support is another important cost factor that is sometimes overlooked. Reliable service from the manufacturer can reduce downtime and help businesses solve operational issues quickly.
Important support services may include:
- Maintenance guidance
- Spare parts availability
- Remote assistance
- Equipment upgrades
- Troubleshooting support
Strong after-sales service adds value throughout the equipment’s service life.
Evaluating Long-Term Return on Investment
The best investment is not always the cheapest option. Businesses should consider how the equipment contributes to:
- Reduced product recalls
- Improved food safety
- Higher production efficiency
- Lower waste levels
- Better compliance with regulations
A reliable metal detection system can provide significant value by protecting both products and brand reputation.
Conclusion
The cost of food metal detection equipment depends on more than the initial purchase price. Factors such as system type, technology, customization, installation, maintenance, and long-term performance all influence the total investment. By carefully evaluating these elements and selecting equipment that matches their production needs, food manufacturers can achieve better safety standards, improved efficiency, and stronger long-term value.


