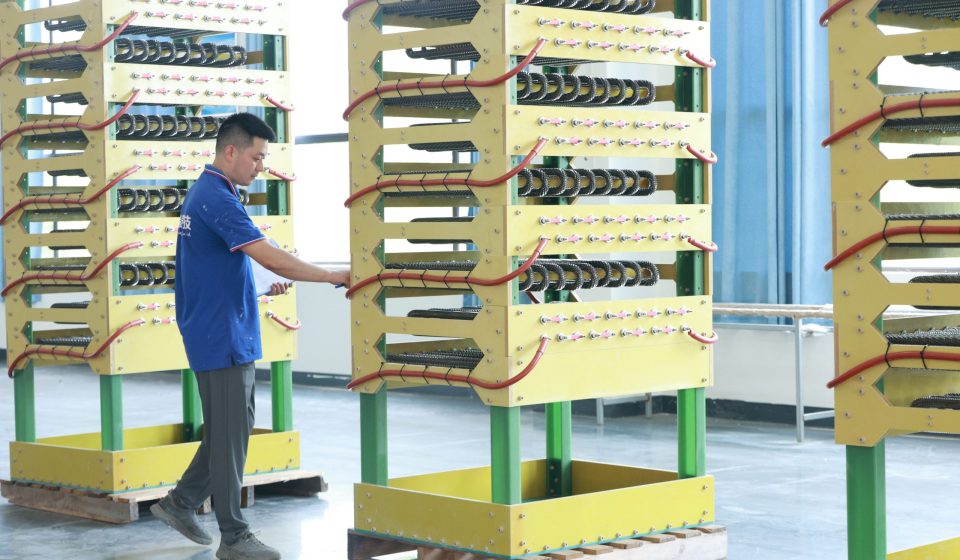

Selecting the right resistive load banks manufacturer is about more than comparing prices or product specifications. The manufacturer you choose should provide reliable equipment, advanced technology, and dependable customer support to ensure accurate and safe power testing. Whether you need load banks for generators, UPS systems, data centers, hospitals, or industrial facilities, choosing a manufacturer with the right capabilities can improve testing efficiency, reduce maintenance costs, and increase the lifespan of your equipment.
Below are the essential features every professional resistive load banks manufacturer should offer.
High-Quality Construction
Durability is one of the most important characteristics of a reliable load bank. A professional manufacturer should use premium materials that can withstand demanding industrial environments and continuous operation.
Look for equipment built with:
- Heavy-duty steel enclosures
- Corrosion-resistant finishes
- Industrial-grade resistor elements
- Durable electrical components
- High-quality insulation materials
Strong construction improves reliability and extends the service life of the load bank.
Wide Range of Power Capacities
Different industries require different testing capacities. A dependable resistive load banks manufacturer should offer products suitable for a variety of applications.
Available options should include:
- Low-capacity portable units
- Medium-capacity industrial models
- High-capacity stationary load banks
- Custom-designed solutions
A broad product range allows customers to select equipment that matches their specific testing requirements.
Customization Options
Every electrical system has unique operational needs. Manufacturers should be able to provide customized load banks that meet project-specific requirements.
Customization may include:
- Various voltage ratings
- Different power capacities
- Indoor or outdoor configurations
- Portable or fixed installations
- Custom control systems
- Specialized enclosure designs
Customized equipment ensures better compatibility with existing power systems.
Advanced Digital Control Systems
Modern load banks should include user-friendly control systems that simplify testing and improve accuracy.
Important digital features include:
- Touchscreen displays
- Programmable testing sequences
- Digital load adjustment
- Real-time monitoring
- Performance reporting
These technologies improve testing efficiency while reducing manual operation.
Reliable Cooling Systems
Since resistive load banks convert electrical energy into heat, efficient cooling is essential for safe and continuous operation.
Manufacturers should provide:
- High-performance cooling fans
- Optimized airflow design
- Temperature monitoring
- Automatic cooling control
- Durable ventilation systems
Effective cooling protects internal components and improves long-term reliability.
Comprehensive Safety Features
Safety should always be a priority during electrical testing.
A professional manufacturer should include features such as:
- Emergency stop buttons
- Over-temperature protection
- Overcurrent protection
- Automatic shutdown systems
- Cooling fan monitoring
- Proper grounding provisions
These safety systems help protect both operators and connected equipment.
Accurate Load Control
Precise load control is essential for obtaining reliable testing results.
Quality load banks should provide:
- Stable load application
- Incremental load adjustments
- Consistent electrical performance
- Accurate power measurement
- Reliable testing under varying conditions
Accurate load simulation helps engineers evaluate equipment performance with confidence.
Factory Testing and Quality Inspection
Every load bank should undergo comprehensive testing before delivery.
A reputable resistive load banks manufacturer should perform:
- Full-load testing
- Functional verification
- Electrical insulation testing
- Cooling system evaluation
- Final quality inspection
Factory-tested equipment minimizes installation issues and ensures dependable operation from day one.
Easy Maintenance Design
Maintenance-friendly equipment reduces downtime and lowers long-term operating costs.
Important design features include:
- Accessible internal components
- Modular construction
- Replaceable resistor elements
- Organized internal wiring
- Easy inspection points
These features simplify servicing and extend equipment life.
Remote Monitoring Capabilities
As industrial automation continues to grow, remote monitoring has become increasingly valuable.
Modern load banks may include:
- Cloud connectivity
- Remote operation
- Live performance monitoring
- Fault notifications
- Data logging
These capabilities allow operators to monitor equipment performance from virtually any location.
Technical Support and Engineering Assistance
The relationship with a manufacturer should continue after the equipment is delivered.
Reliable support services include:
- Product selection guidance
- Installation recommendations
- Technical consultations
- Troubleshooting assistance
- Maintenance advice
- Spare parts support
Strong technical support helps customers maximize the value of their investment.
Fast Delivery and Production Capacity
Project schedules often depend on timely equipment delivery.
An experienced manufacturer should have:
- Efficient production facilities
- Reliable inventory management
- Flexible manufacturing capacity
- Ability to meet urgent project deadlines
Consistent delivery performance helps customers complete projects on schedule.
Compliance with International Standards
Manufacturers should follow recognized quality and safety practices throughout the production process.
Compliance demonstrates a commitment to:
- Consistent manufacturing quality
- Reliable product performance
- Safe equipment operation
- Continuous quality improvement
Customers gain greater confidence when purchasing equipment built according to internationally accepted standards.
Long-Term Product Reliability
A quality load bank should deliver dependable performance throughout many years of operation.
Reliable equipment provides:
- Reduced maintenance requirements
- Lower operating costs
- Consistent testing accuracy
- Extended service life
- Improved return on investment
Manufacturers that prioritize reliability help customers avoid costly equipment failures.
Conclusion
Choosing the right resistive load banks manufacturer involves evaluating far more than product specifications. High-quality construction, customization options, advanced digital controls, efficient cooling systems, comprehensive safety features, accurate load control, factory testing, maintenance-friendly design, remote monitoring, and dependable technical support are all essential characteristics of a trusted manufacturer. By selecting a manufacturer that offers these features, businesses can ensure reliable power testing, reduce operational risks, improve maintenance efficiency, and achieve long-term value from their investment in resistive load bank equipment.