
Purchasing a liquid cooled load bank for the first time is an important investment for any organization involved in power generation, data centers, renewable energy, marine operations, or industrial testing. The quality of the manufacturer you choose directly affects the reliability, safety, and long-term performance of your testing equipment. A professional liquid cooled load banks manufacturer should provide more than just quality products—they should offer engineering expertise, customization, technical support, and dependable after-sales service. This guide highlights the key factors first-time buyers should consider before making a purchasing decision.
The first step is understanding your testing requirements. Before contacting a liquid cooled load banks manufacturer, determine the type of equipment you need to test, including generators, uninterruptible power supplies (UPS), battery energy storage systems, or renewable energy installations. Consider your required voltage, frequency, power capacity, duty cycle, and testing environment. Clearly defining these requirements helps manufacturers recommend the most suitable solution.
Industry experience is another critical factor. Manufacturers with years of experience have a better understanding of different industries and testing applications. An experienced company is more likely to have successfully completed projects for data centers, power plants, marine facilities, and industrial operations. Their knowledge enables them to provide practical recommendations and reliable equipment that meets demanding operational requirements.
Product quality should always be a top priority. A reliable liquid cooled load banks manufacturer uses premium materials, high-quality electrical components, durable cooling systems, and precision manufacturing processes. Well-built equipment delivers consistent performance, requires less maintenance, and provides a longer operational lifespan. Buyers should also ask about the manufacturer’s quality control procedures and factory testing process.
Customization capabilities are equally important. Every project has unique technical requirements, and standard products may not always provide the best solution. A professional manufacturer should be able to customize voltage ratings, power capacities, control systems, cooling configurations, communication interfaces, and enclosure designs to match specific customer needs. Customized solutions improve system compatibility and operational efficiency.
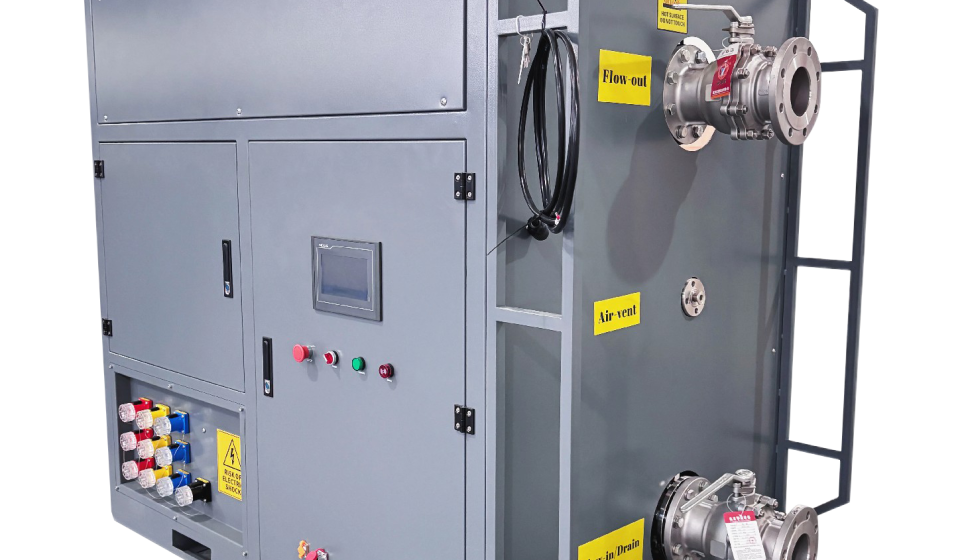
The cooling system deserves careful attention because it directly affects equipment performance. Liquid cooled load banks rely on efficient coolant circulation to remove heat generated during testing. Buyers should evaluate how the liquid cooled load banks manufacturer designs its cooling system, including coolant flow management, heat exchanger efficiency, leak prevention measures, and thermal monitoring capabilities. An effective cooling system supports reliable operation during extended high-load testing.
Modern control systems provide significant operational advantages. Many advanced load banks include programmable controllers, touchscreen displays, automated testing functions, remote monitoring, and data logging capabilities. These features improve testing accuracy, simplify operation, and provide valuable performance information for maintenance planning and reporting.
Safety should never be overlooked. A trustworthy liquid cooled load banks manufacturer incorporates multiple protective features such as overcurrent protection, overtemperature monitoring, emergency stop buttons, coolant flow detection, fault alarms, electrical grounding, and automatic shutdown systems. These safety measures protect both operators and connected equipment during testing operations.
Maintenance requirements also influence long-term ownership costs. Maintenance-friendly designs feature accessible service panels, modular components, clearly labeled wiring, and simplified coolant servicing. Easy access to critical components reduces maintenance time, lowers labor costs, and minimizes equipment downtime throughout the product’s lifecycle.
Technical support and after-sales service are just as important as the equipment itself. First-time buyers often require assistance during installation, commissioning, operator training, troubleshooting, and routine maintenance. A dependable liquid cooled load banks manufacturer should provide responsive technical support, detailed documentation, spare parts availability, and ongoing service throughout the equipment’s operational life.
It is also wise to evaluate the manufacturer’s production capabilities. Companies with advanced manufacturing facilities, modern production equipment, and comprehensive testing laboratories are generally better equipped to maintain consistent product quality. Factory testing should include electrical verification, insulation testing, coolant system inspections, safety checks, and full-load performance evaluations before shipment.
Cost should be considered carefully, but it should not be the only deciding factor. While lower-priced equipment may appear attractive initially, it can result in higher maintenance expenses, reduced reliability, and shorter service life. Focusing on overall value—including product quality, performance, support, and durability—often leads to a better long-term investment.
Finally, consider the manufacturer’s commitment to innovation. The power industry continues to evolve with growing demand for AI data centers, renewable energy systems, and high-density electrical infrastructure. Manufacturers that invest in research and development are more likely to offer advanced technologies, improved energy efficiency, intelligent monitoring systems, and future-ready solutions that support changing industry needs.
In conclusion, selecting the right liquid cooled load banks manufacturer requires careful evaluation of experience, product quality, customization, safety, cooling technology, maintenance, technical support, manufacturing capabilities, and long-term value. By taking the time to assess these factors, first-time buyers can confidently invest in reliable equipment that delivers accurate testing, dependable performance, and lasting operational benefits for years to come.